Pharma operations and supply chain management are converging with forecasting, manufacturing, resilience, and digitalisation of Technical Operations.
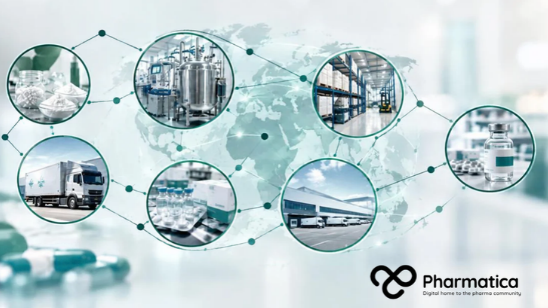
Pharma operations and supply chain management depend on how well manufacturers connect demand, production, suppliers, inventory, logistics, technology, and risk.
In modern operations these functions cannot be managed as isolated activities, and that creates important implications for Technical Operations.
Image
Pharma Operations and Supply Chain Management as One System
Pharmaceutical supply chains are difficult to manage because they combine long lead times, strict quality requirements, complex manufacturing processes, specialised suppliers, regulatory obligations, and highly variable demand.
A disruption in one part of the system can therefore affect production, inventory, distribution, and ultimately medicine availability.
The principles, practices, technologies, and strategies shaping contemporary operations and supply chain management are constantly being updated.
Technical Operations have to connect manufacturers, distributors, procurement organisations, and healthcare providers within a wider flow of products, information, services, and resources.
This means that supply chain performance is not separate from manufacturing performance. The two systems influence each other continuously.
That changes how Technical Operations leaders need to think about supply chain resilience.
A supplier problem can become a manufacturing problem; a manufacturing delay can become an inventory problem; an inventory shortage can become a distribution problem, and a forecasting error can propagate across all three.
This interconnectedness makes end-to-end visibility increasingly important.
Forecasting Errors Travel Through the Supply Chain
Demand forecasting sits at the centre of operational planning because decisions about production, purchasing, inventory, capacity, and sourcing all depend on expectations about the future.
Firstly, Technical Operations teams need to understand the important distinction between a forecast and a target.
A forecast describes what may happen, while a target describes what an organisation wants to happen. Confusing the two can create operational decisions based on ambition rather than evidence.
This is vitally important in pharmaceutical supply chains.
A medicine may have an expected demand curve based on epidemiology, market access, prescribing behaviour, clinical uptake, seasonality, or competitor activity. Commercial teams may simultaneously establish growth targets that sit above that forecast.
Manufacturing and supply chain teams must understand the difference.
If production plans are built around optimistic targets rather than realistic demand signals, organisations can carry unnecessary inventory or create capacity that is not needed. If forecasts are too conservative, manufacturers may struggle to respond when demand rises.
Teams must also understand the bullwhip effect, where relatively small changes in downstream demand become much larger fluctuations in upstream orders.
It can be very startling to realise how substantial this amplification can become.
A review of supply chain management found that in one UK grocery chain example, production-order variance was 7.68 times demand variance. In a US information-technology consumables example, shipment variance was 3.58 times the variance in factory demand.
These examples are not pharmaceutical measurements, but the principle is highly relevant to pharma supply networks.
A manufacturer receiving increasingly volatile forecasts from distributors, affiliates, or commercial functions may respond by changing production schedules, safety stocks, procurement orders, or capacity plans.
The original demand signal can become progressively distorted as it moves upstream.
For pharmaceutical organisations, this creates several priorities:
Improve the quality and frequency of demand signals.
Separate commercial targets from operational forecasts.
Connect forecasting with inventory and production planning.
Monitor variability across multiple tiers rather than focusing only on direct suppliers.
The objective is to prevent uncertainty from becoming unnecessary operational volatility.
“This is one of the riskiest industries there is because you're dealing with human lives, you're dealing with experimental protocols, and you're dealing with regulatory bodies where you might not get another shot at that clinical trial."
Image
Supply Chain Resilience Requires More Than Extra Inventory
Pharma supply chain resilience has traditionally been associated with buffers, alternative suppliers, additional capacity, and contingency planning.
Those remain important, but resilience is actually a broader systems issue.
To strengthen resilience in healthcare and pharmaceutical supply chains, the focus should be on building flexibility, redundancy, collaboration, and agility.
In pharma supply chain optimisation, the focus can extend to shorter delivery times, localised sourcing, and moving production closer to the point of care or a trial site.
For pharmaceutical manufacturers, each approach creates different trade-offs.
Redundancy can mean qualifying additional suppliers or maintaining additional capacity. This can reduce dependence on a single source but may increase cost.
Flexibility can involve adaptable manufacturing platforms, alternative production routes, or facilities capable of handling changing product requirements.
Collaboration can improve information sharing between manufacturers, suppliers, distributors, and healthcare organisations.
Agility focuses on how quickly the network can respond when conditions change.
These capabilities become particularly important for products with complex manufacturing requirements.
Then there is the difficult question of localisation.
Moving production and sourcing closer to markets can reduce exposure to long global supply chains. However, localisation requires investment in facilities, labour, infrastructure, and technical knowledge. It can also create regulatory complications when products move across jurisdictions.
In summary, supply chain resilience cannot be reduced to a single metric such as inventory days or supplier count.
A resilient network needs options.
Image
Digitalisation Connects Manufacturing With the Wider Network
Digitalisation is another major theme running through modern operations and supply chain management.
In pharmaceutical manufacturing, digital systems can connect production data with quality, inventory, procurement, maintenance, logistics, and demand information.
That creates opportunities to move from fragmented operational decisions towards a more connected model.
This is already visible in the development of digital manufacturing, process analytical technology, electronic records, predictive maintenance, and advanced analytics.
The value of digitalisation, however, does not come simply from collecting more data.
A connected supply chain requires consistent data, interoperable systems, clear ownership, and decision processes that can act on the information generated.
This is especially important when pharmaceutical organisations operate across multiple manufacturing sites and external partners.
A CDMO (Contract Development Manufacturing Organsation) may hold manufacturing data and a raw-material supplier may hold information about upstream availability. A logistics provider may hold shipment data, while a commercial organisation may own demand information.
If these systems remain disconnected, the organisation can still have enormous amounts of data without having genuine supply chain visibility.
That makes digital integration an important operational capability.
Healthcare Supply Chains Put Operational Decisions in Context
The healthcare sector is an important reminder that supply chain performance ultimately affects service delivery and patient outcomes.
Healthcare supply chain management involves manufacturers, distributors or wholesalers, and service providers or procurement organisations.
In the healthcare sector, the objective is not simply to move products efficiently, but to coordinate people, processes, information, and finances while controlling cost and supporting healthcare delivery.
For pharma, that creates a broader definition of operational performance.
A factory can meet its production target while the wider supply chain still experiences shortages.
A supplier can deliver materials on time while a logistics disruption prevents medicines from reaching a market.
An inventory reduction programme can improve working capital while increasing exposure to an unexpected disruption.
This is why supply chain decisions increasingly need to be evaluated against the complete product lifecycle.
The pharmaceutical supply chain also operates within a regulatory environment that can make rapid structural changes difficult.
Different countries can impose different requirements on manufacturing, procurement, quality, and distribution. These differences can complicate localisation decisions and contribute to inefficiencies, including shortages.
For global pharmaceutical organisations, resilience therefore depends on balancingefficiency, regulatory requirements, flexibility, cost, and continuity of supply.
AI in Pharma: Why the Future of Healthcare Starts With Patients, Not Tech
Kate O’Reilly, President & Chair of the Healthcare Businesswomen’s Association (HBA) Dublin-Ireland Chapter & Healthcare Transformation Partner at Roche, discusses AI in pharma, patient engagement, and the future of healthcare innovation.
Image
What the Operations Model Means for Pharma Supply Chains
A pharmaceutical operating model for supply chain management points towards several actions for Technical Operations to take.
First, supply chain strategy should be connected to manufacturing strategy. Procurement, production, quality, logistics, and commercial planning should not operate as independent optimisation exercises.
Forecasting also needs to be treated as an enterprise capability. Poor forecasts can create unnecessary variability that becomes increasingly expensive as it moves upstream.
Additionally, resilience should be designed rather than added after disruption occurs. Supplier diversity, flexible capacity, alternative routes, inventory buffers, and scenario planning all have a role, but their value depends on how they interact.
Fourth, digitalisation should focus on decision quality. More systems and more data do not automatically produce greater visibility.
Finally, supply chain teams need to measure operational performance across the network rather than at individual points.
The strongest supply chain is the one that can absorb disruption, maintain quality, adapt capacity, and continue supplying patients without creating unnecessary structural cost.
That is the role of Technical Operations.
Image
Building a More Connected Pharma Supply Chain
A shift is already visible across pharmaceutical manufacturing. Supply chains are becoming more connected, more data-intensive, and more exposed to disruption.
The pharmaceutical sector cannot remove uncertainty from demand, geopolitics, manufacturing, logistics, or supplier networks. It can, however, build systems that respond to uncertainty more effectively.
For pharma operations and supply chain management, that means connecting forecasting with production, production with suppliers, suppliers with risk management, and operational data with decision-making.
The result is a more efficient supply chain with a more adaptable pharmaceutical operating system, capable of protecting continuity while supporting the increasingly complex products entering the market.
At Pharmatica, we examine the systems, strategies, and technologies shaping pharmaceutical Technical Operations. Our Insights and expert analysis connect manufacturing, supply chain, quality, and operational resilience to the decisions that determine how reliably medicines move from production to patients.
Pharmatica: Insight. Connection. Impact.
Frequently Asked Questions
What is pharma operations and supply chain management?
Pharma operations and supply chain management covers the connected activities required to plan, manufacture, store, distribute, and supply pharmaceutical products. It includes demand forecasting, procurement, production, inventory, quality, logistics, supplier management, and risk management.
Why is supply chain management important in pharmaceutical manufacturing?
Pharmaceutical supply chain management helps manufacturers maintain reliable access to materials, production capacity, and distribution while controlling cost and protecting product quality. Because pharmaceutical manufacturing often involves specialised suppliers, long lead times, regulatory requirements, and temperature-sensitive products, disruption at one point can affect the wider supply network.
How can pharmaceutical companies improve supply chain resilience?
Pharmaceutical companies can improve supply chain resilience through supplier diversification, alternative manufacturing capacity, better demand forecasting, strategic inventory, supply chain visibility, scenario planning, and stronger collaboration with suppliers and logistics partners. Resilience also depends on the ability to respond quickly when disruptions occur.
What is the bullwhip effect in pharmaceutical supply chains?
The bullwhip effect occurs when relatively small changes in customer or market demand create progressively larger fluctuations in orders further upstream. In pharmaceutical supply chains, inaccurate forecasts, changing commercial assumptions, long lead times, and inventory policies can amplify demand variability and make production and procurement planning more difficult.
How is digitalisation changing pharmaceutical supply chain management?
Digitalisation is connecting manufacturing, inventory, procurement, logistics, quality, and demand information more closely. Digital platforms, analytics, connected equipment, predictive technologies, and integrated data systems can improve supply chain visibility and support earlier decision-making. The value depends on reliable data, interoperable systems, governance, and the ability to act on operational information.
Nicole (BSc Molecular Medicine, Honours Medical Biochemistry) has many years of pharmaceutical experience, having worked for top CROs and biopharma companies for more than a decade.
Did you enjoy the content?
0
Why not support
Nicole Dale
by giving this content a like
What 13 Years of Data Shows About Drug Innovation in Psychiatry
From 2012 through 2024, the FDA only approved 22 drugs for the treatment of psychiatric conditions. Pharma R&D teams must rethink development strategies to unstall drug innovation in psychiatry
Pharmacoinformatics is redefining drug discovery strategy. This analysis covers the AI platforms, molecular design tools, and regulatory frameworks shaping R&D pipelines in 2026.
Why Precision Alone Isn't Enough in Oncology Drug Discovery
Precision alone isn’t enough in oncology drug discovery. See why execution, biomarkers, and trial design determine scalable success in precision medicine.
Phenotypic drug discovery is reshaping how pharma finds first-in-class drugs. This analysis covers the methods, AI integration, and strategic decisions R&D leaders face in 2026.
Learn how drug discovery scientists are evolving alongside AI, computational biology, and multidisciplinary research to accelerate therapeutic innovation.


Comments (0)